Language
 English
 русский
 Español
Get A Quote
Get A Quote
 Home / Equipment / DM Desktop Pedal Spot Welding Machine / DM1-5KW Customizable Desktop Pedal Precision Welding Machine

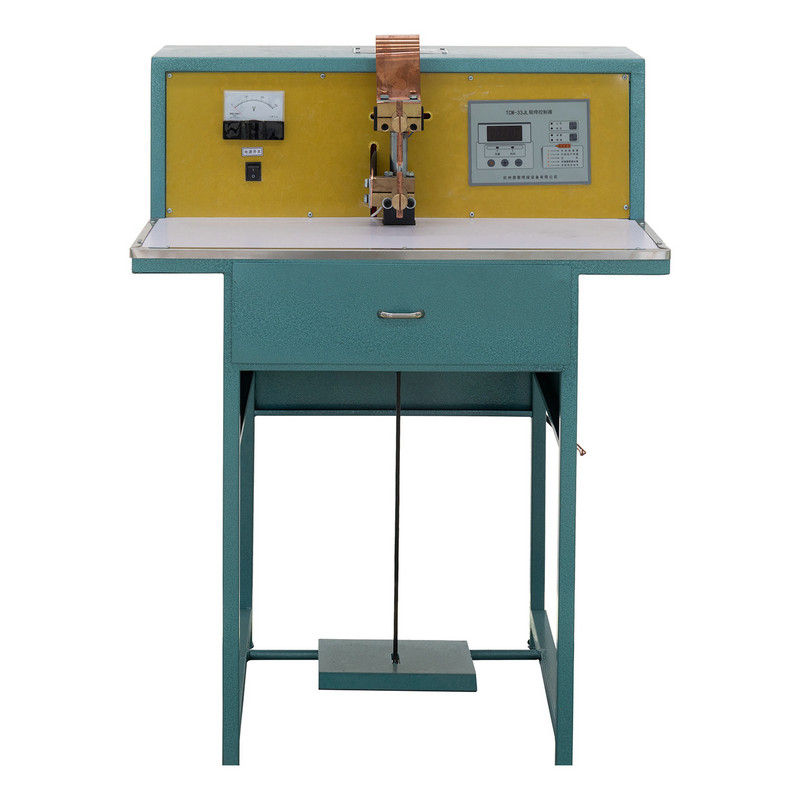
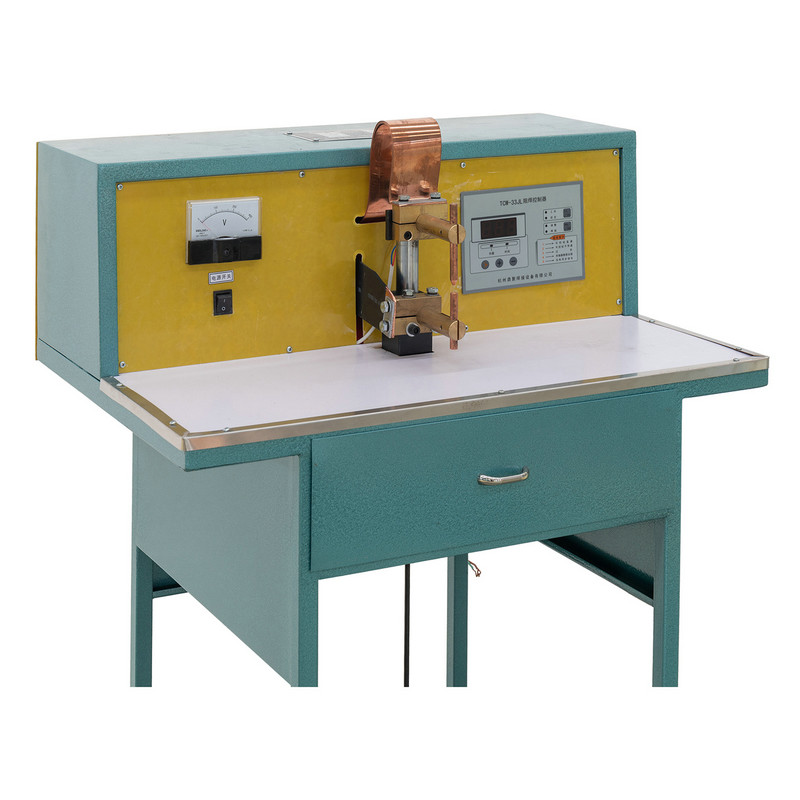
DM1-5KW Customizable Desktop Pedal Precision Welding Machines, these units feature a pedal pressure design that boasts user-friendliness, robust construction, and longevity. Integrated circuits play a pivotal role in regulating the heat and timing of the primary circuit, ensuring precision during operation. Leveraging the power frequency cycle of 50HZ, the welding machines execute accurate counting control and precise time management. Across industries such as metalwork, electrical instrumentation, automotive manufacturing, shipbuilding, and aviation, these welding machines are indispensable for joining materials like low-carbon steel and stainless steel in industrial processes. Their versatility and reliability make them a staple in major manufacturing sectors.

Specifications
|
Model |
Unit |
DM1-16KW |
|
|
Primary voltage |
V |
380 |
|
|
Rated capacity |
KVA |
16 |
|
|
Rated primary current |
A |
42 |
|
|
Rated load duration |
% |
20 |
|
|
No load voltage |
V |
0.2-2.9 |
|
|
Extension length of electrode arm |
mm |
100 |
|
|
Distance between electrode arms |
mm |
80 |
|
|
Working stroke of upper electrode |
mm |
20 |
|
|
Maximum pressure between electrodes |
N |
600 |
|
|
Electrode size |
Electrode arm |
mm |
Ф22 |
|
Electrode holder |
mm |
Ф10 |
|
|
Welding thickness |
Low carbon steel |
mm |
2+2 |
|
Cooling water flow |
L/min |
2 |
|
Product Description
Master the art of precision welding with the DM1-5KW, a robust and user-friendly desktop pedal welding machine engineered for industrial-grade performance. Designed for versatility and control, this machine is the ideal solution for workshops and production lines requiring reliable, high-quality spot welding for a wide range of applications. Its customizable nature ensures it can be tailored to meet your specific operational needs.
The DM1-5KW Precision Welding Machine is a staple tool in numerous industries where reliable metal joining is critical. Its primary applications include:
Recommended Products
KEEP IN TOUCH
Picture a mild steel bracket that cracks at the weld after a few months of vibration. The material looks correct, the rod was forgotten in a damp drawer, and the welder ran a long arc at 160 A. The f...
READ MORE
Your new MIG unit runs well for the first hour. Then the arc begins to sag, spatter builds up, and the machine trips out. You replace the contact tip, check the gas, and clean the liner, but the prob...
READ MOREYou are rewiring a production cell to join steel rods before drawing or straightening. The two candidate machines on the quote are a flash butt welding machine and a regular butt welding machine. Bot...
READ MORE
Oxygen Hose Color: The Direct Answer Walk onto any welding floor in the U.S. and you will see a green hose connected to an oxygen regulator. In Europe, the same gas hose is blue. Both are correct und...
READ MORE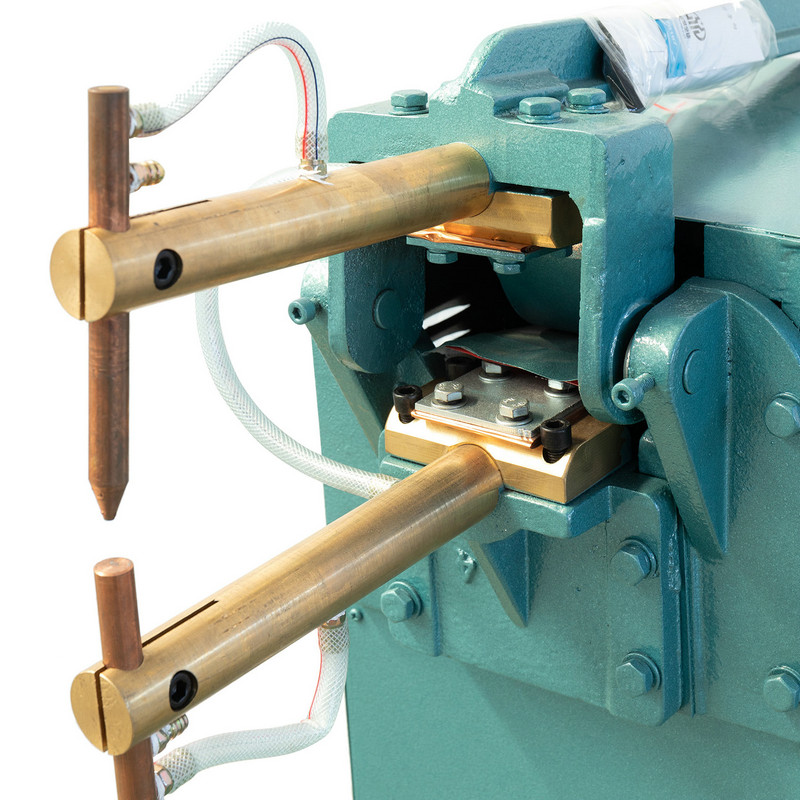
Your sheet metal line is producing inconsistent welds. It may not be the operator's technique. More often, the machine was never matched to the actual job. Before replacing anything, it helps to star...
READ MORE
Why Pipe Cutting Automation Is a Production Decision, Not Just a Tool Purchase In shops that fabricate pipe or tube, the cutting stage is where schedules are lost. An operator measures a length, mark...
READ MORE
Product
Contact Info.
+86-152-5712-5882
Fax: +86-563-2269966
No. 21 Guangping Road, Guangde Economic Development Zone, Guangde City, Anhui Province
QR Code