Language
 English
 русский
 Español
Get A Quote
Get A Quote
 Home / Equipment / DN Pedal Spot Welding Machine / DN3 Pneumatic Pedal Spot Welding Machine / DN3-40KW Metal Shell Digital Display Pneumatic Pedal Spot Welding Machine

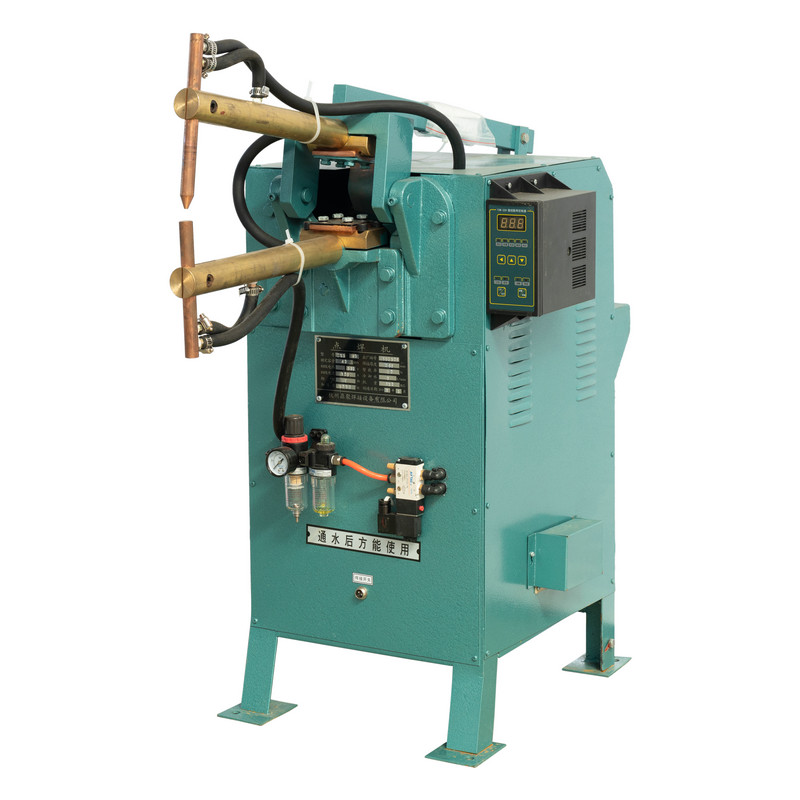
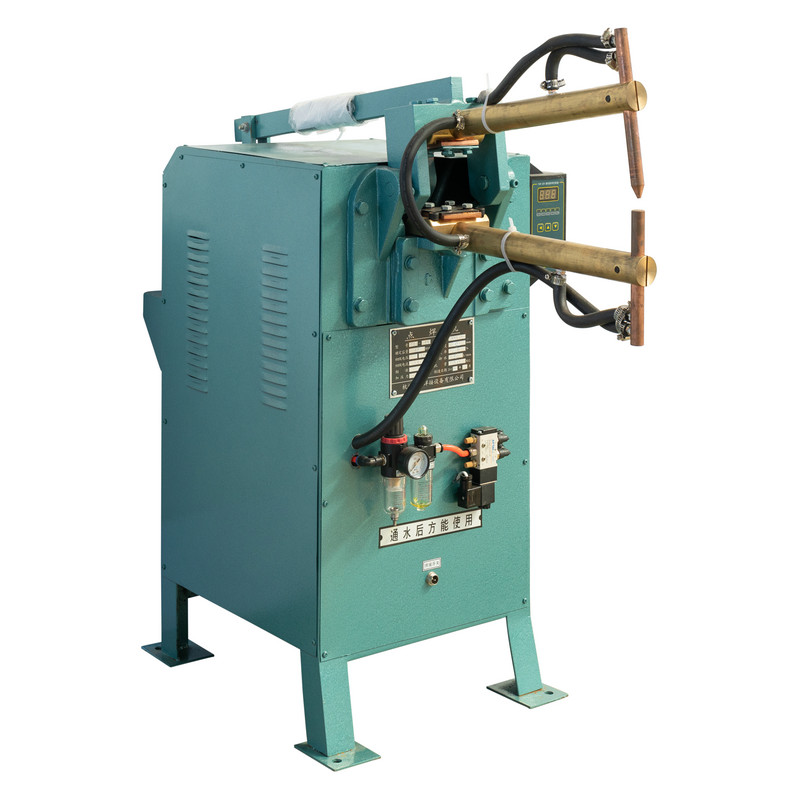
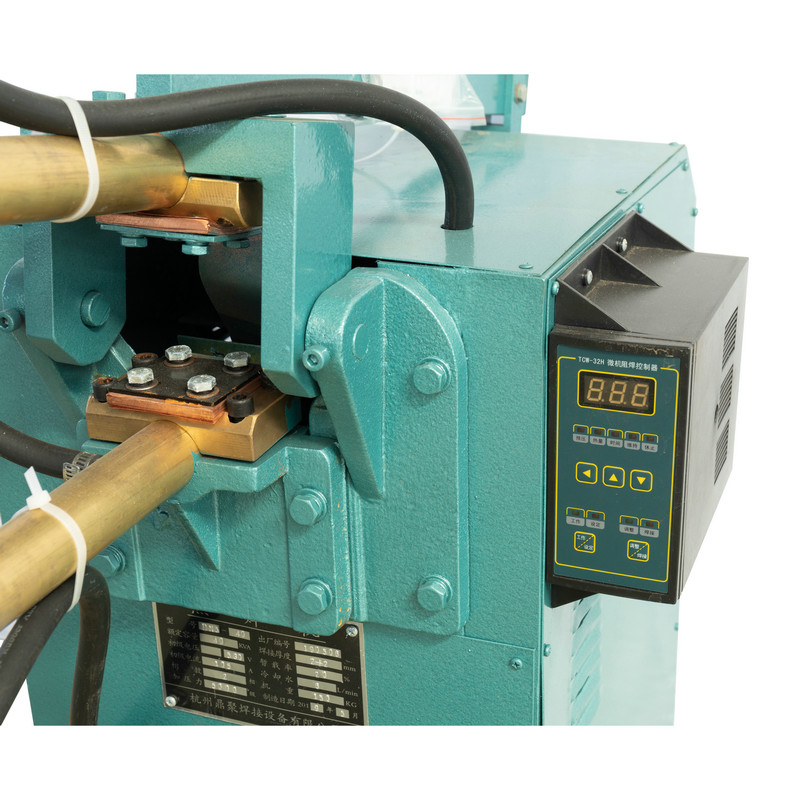
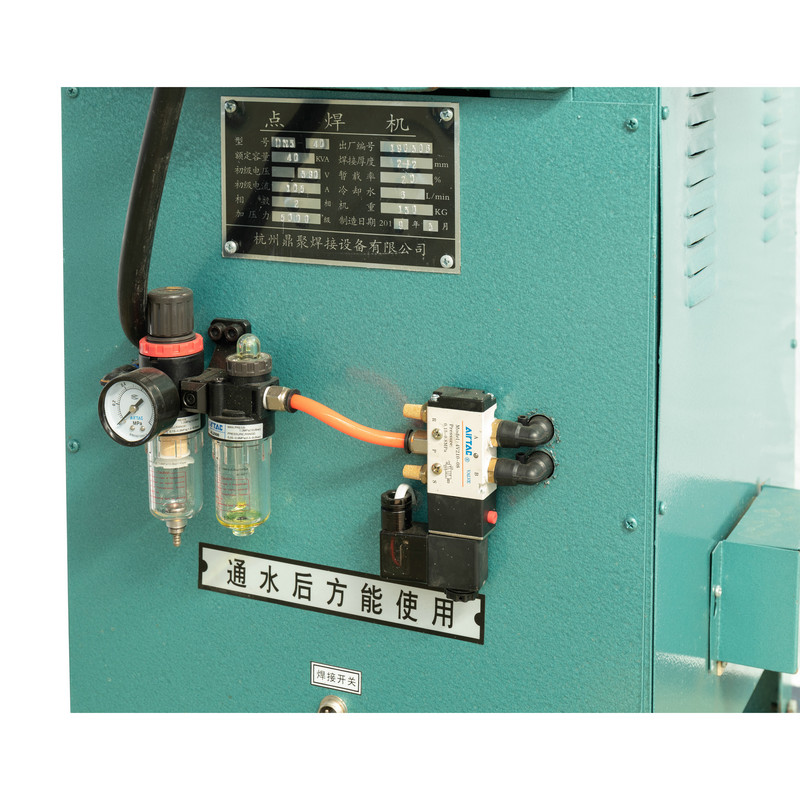
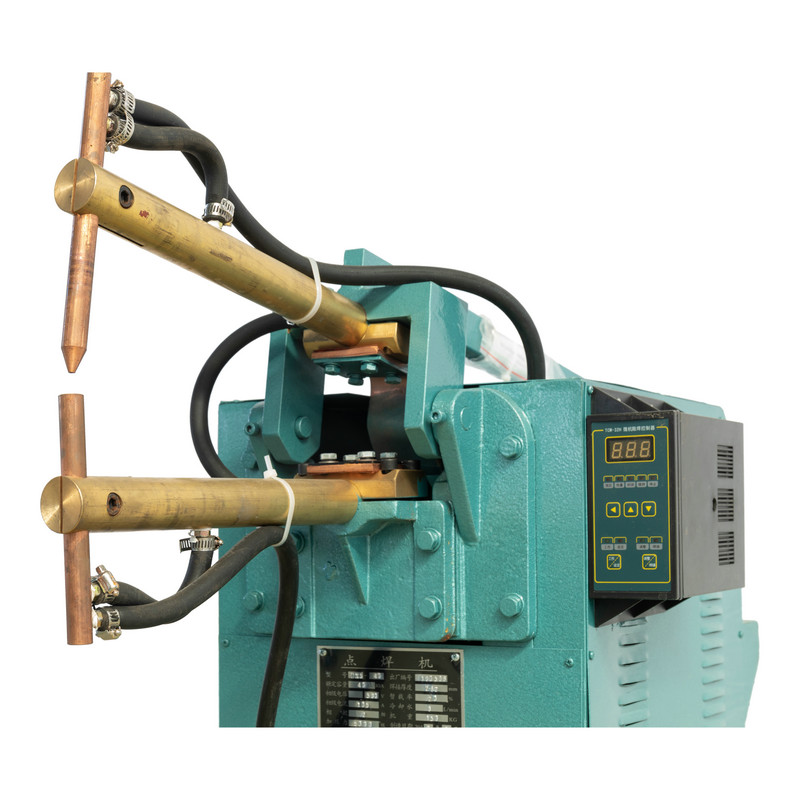
DN3-40KW Metal Shell Digital Display Pneumatic Pedal Spot Welding Machine uses high-quality semiconductor components such as thyristors and integrated blocks to form a control circuit. It can accurately adjust and control the welding current and time. It is suitable for thin plates, wire mesh, cabinets, security doors, automobile repair, etc. Welding of steel furniture, stainless steel products, air conditioning equipment, etc. The main transformer has low power consumption, small no-load current, small size, and is easy to operate and transport.

Specifications
|
Model |
Unit |
DN3-25KW |
DN3-40KW |
|
|
Primary voltage |
V |
380 |
380 |
|
|
Rated frequency |
HZ |
50 |
50 |
|
|
Rated capacity |
KVA |
25 |
40 |
|
|
Rated primary current |
A |
65 |
105 |
|
|
Rated load duration |
% |
20 |
20 |
|
|
No load voltage |
V |
0.5-3.2 |
0.5-3.58 |
|
|
Extension length of electrode arm |
mm |
300 |
300 |
|
|
Distance between electrode arms |
mm |
200 |
200 |
|
|
Working stroke of upper electrode |
mm |
40 |
40 |
|
|
Maximum pressure between electrodes |
N |
1000 |
1000 |
|
|
Electrode size |
Electrode arm |
mm |
Ф40 |
Ф40 |
|
Electrode holder |
mm |
Ф20 |
Ф20 |
|
|
Electrode head |
mm |
Ф13 |
Ф13 |
|
|
Welding thickness Low carbon steel |
mm |
2+2 |
2.5+2.5 |
|
|
Adjusting series |
- |
Stepless voltage regulation |
Stepless voltage regulation |
|
Product Description
The primary differences between the two models are:
Both models share several identical specifications, indicating common design elements and features:
The DN3-40KW is a more powerful version of the DN3-25KW, capable of handling thicker materials due to its increased rated capacity and primary current. Otherwise, many of their mechanical and operational specifications are identical, suggesting they are part of the same product family with power output being the primary differentiator.
Recommended Products
KEEP IN TOUCH
Picture a mild steel bracket that cracks at the weld after a few months of vibration. The material looks correct, the rod was forgotten in a damp drawer, and the welder ran a long arc at 160 A. The f...
READ MORE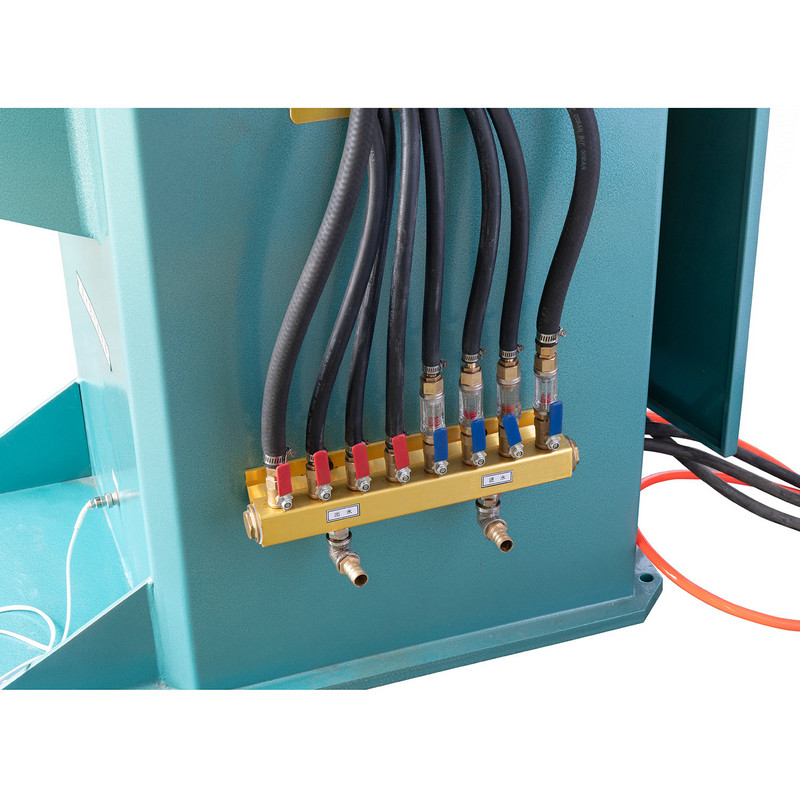
Your new MIG unit runs well for the first hour. Then the arc begins to sag, spatter builds up, and the machine trips out. You replace the contact tip, check the gas, and clean the liner, but the prob...
READ MOREYou are rewiring a production cell to join steel rods before drawing or straightening. The two candidate machines on the quote are a flash butt welding machine and a regular butt welding machine. Bot...
READ MORE
Oxygen Hose Color: The Direct Answer Walk onto any welding floor in the U.S. and you will see a green hose connected to an oxygen regulator. In Europe, the same gas hose is blue. Both are correct und...
READ MORE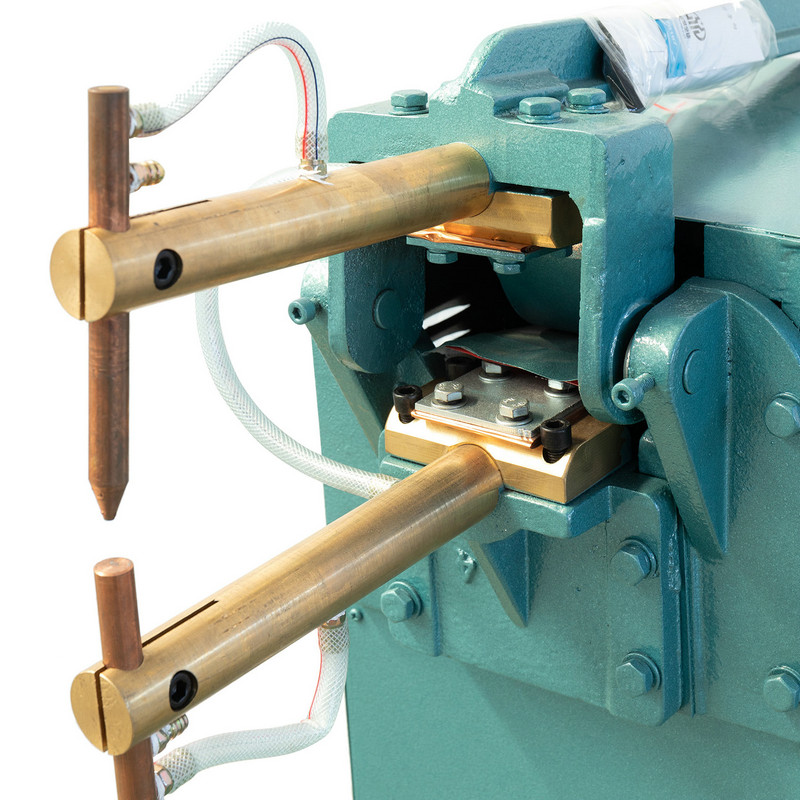
Your sheet metal line is producing inconsistent welds. It may not be the operator's technique. More often, the machine was never matched to the actual job. Before replacing anything, it helps to star...
READ MORE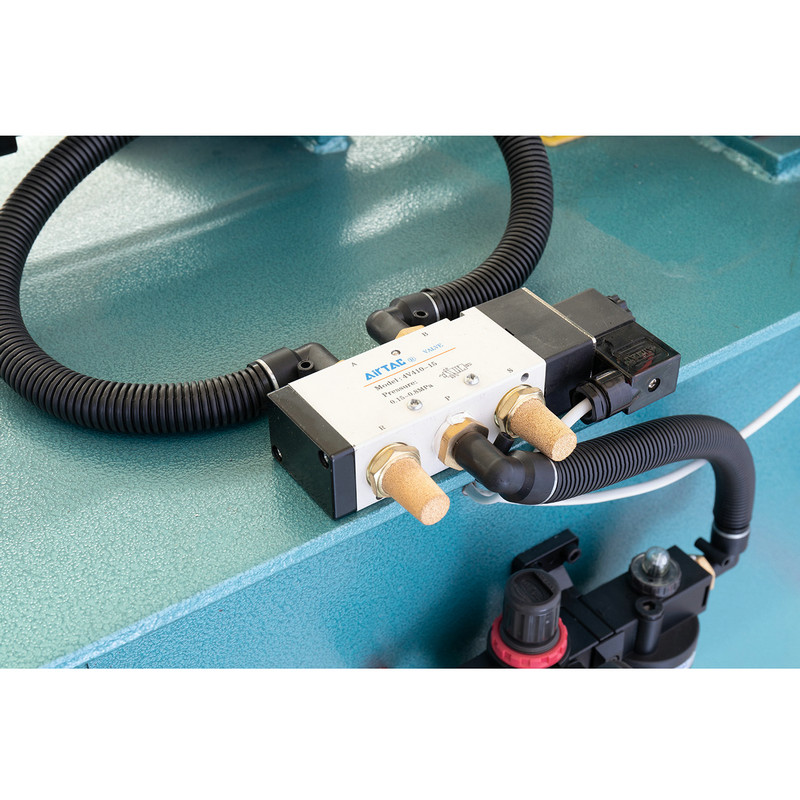
Why Pipe Cutting Automation Is a Production Decision, Not Just a Tool Purchase In shops that fabricate pipe or tube, the cutting stage is where schedules are lost. An operator measures a length, mark...
READ MORE
Product
Contact Info.
+86-152-5712-5882
Fax: +86-563-2269966
No. 21 Guangping Road, Guangde Economic Development Zone, Guangde City, Anhui Province
QR Code